Key takeaways
- Winding temperature defines transformer life expectancy because every 6°C to 7°C increase above thermal limits cuts paper insulation life by half.
- Standard IEC 60076-2 limits the average transformer winding temperature rise to 65 K for standard mineral oil systems with a maximum hot-spot rise of 78 K.
- Conventional winding temperature indicators (WTI) do not directly measure copper temperature; they simulate it using top oil temperature plus a CT-driven heater coil.
- Direct fibre-optic temperature probes installed within winding spacers eliminate the simulation lag of WTIs and are essential for high-overload renewable applications.
- During factory heat run tests per IEC 60076-2 Clause 7, winding resistance must be logged across shutdown and mathematically extrapolated back to zero time.
Quick answer: Transformer winding temperature represents the internal thermal stress on the copper or aluminium conductors and solid insulation, serving as the primary physical limiter of electrical capacity. Exceeding rated thermal limits accelerates the chemical breakdown of cellulose insulation, halving operational lifespan for every 6°C to 7°C increase above design thresholds.
In electrical power networks, the thermal performance of a transformer directly dictates its continuous current-carrying capability, peak overload tolerance, and total service longevity. While structural steel, mineral oil, and porcelain or polymer components withstand relatively high temperatures without rapid mechanical failure, solid dielectric materials—specifically kraft paper, creped paper, and pressboard—suffer irreversible depolymerisation when subjected to sustained elevated thermal stress. Operating engineers, substation designers, and procurement managers must understand how internal heat is generated, transferred, monitored, and specified across standard operating regimes.
Thermal management requires balancing electrical load losses, environmental conditions, and mechanical cooling efficiency. Managing this balance ensures that peak copper temperatures remain strictly within defined boundaries established by international regulatory frameworks such as IEC and IEEE. Failure to control thermal accumulation leads directly to dielectric breakdown, gassing in liquid-filled units, turn-to-turn flashovers, and catastrophic fleet outages.
Understanding Transformer Winding Temperature and Hot Spots
Internal transformer temperature varies considerably across the height and cross-section of the core-and-coil assembly rather than remaining uniform throughout the tank.
Heat generation within an energised transformer originates from two fundamental mechanisms: no-load losses (core hysteresis and eddy currents in the electrical steel laminations) and load losses (ohmic $I^2R$ resistance and stray eddy currents in the winding conductors and structural steel clamping plates). Because the electrical current flows directly through the winding conductors, the copper or aluminium turns represent the most concentrated internal thermal source.
Cooling medium dynamics create a distinct thermal gradient within the tank. In a standard liquid-immersed transformer, cooling fluid enters the bottom of the winding ducts at its lowest temperature, absorbs thermal energy as it ascends via thermo-siphon or pumped circulation, and exits at the top. Consequently, top oil temperature is consistently higher than bottom oil temperature. However, the conductor metal is separated from the bulk oil by several millimetres of electrical paper insulation, creating a thermal boundary layer.
Engineers classify internal heat into three primary metrics:
- Top Liquid (Oil) Temperature: The temperature of the insulating fluid gathered at the top of the tank before it enters radiators or heat exchangers.
- Average Winding Temperature: The mean temperature of the entire metallic winding circuit, historically calculated during factory testing by measuring the change in direct-current resistance from cold conditions.
- Hot-Spot Winding Temperature: The peak localised temperature occurring within the winding structure, typically located between 70% and 90% of the winding height where the ambient oil is already hot and stray magnetic leakage flux concentrates at the winding extremities.
The winding hot spot ($T_{hs}$) represents the limiting operational parameter. While the average transformer winding temperature may appear safe on an analogue dashboard, an unmonitored hot spot can simultaneously exceed thermal endurance limits, degrading dielectric paper at a rapid rate.
Transformer Temperature Rise Limits According to Standards
International standards govern thermal design by defining maximum allowable transformer temperature rise above specified ambient air baselines rather than setting simple absolute ceiling values.
Temperature rise represents the differential between the energised component and the external cooling ambient. IEC 60076-2 Clause 4.1 establishes standard ambient conditions: maximum ambient temperature of 40°C, a monthly average of 30°C in the hottest month, and an annual average of 20°C. Conversely, IEEE C57.12.00 Clause 5.1 defines ambient baselines with a 40°C maximum and a 30°C daily average. If the destination site exceeds these standard ambients—such as desert substations operating at 50°C—the permissible rise must be de-rated to prevent premature thermal ageing.
Thermal endurance classes depend on the fluid and insulation system selected. Standard non-upgraded kraft paper corresponds to an IEC Class A system (105°C maximum operating limit). Thermally upgraded paper (chemically treated with dicyandiamide or melamine) allows higher operating temperatures, raising the reference hot-spot endurance limit to 110°C or 120°C depending on the standard adopted.
The table below provides a concrete comparison of permissible transformer temp rise limits across dominant international design standards for mineral-oil and dry-type units:
| Standard & Class | Cooling / Insulation Medium | Top Liquid Rise Limit (K) | Average Winding Rise Limit (K) | Hot-Spot Rise Limit (K) | Max Continuous Hot-Spot (°C) |
|---|---|---|---|---|---|
| IEC 60076-2 (Standard Paper) | Mineral Oil | 60 | 65 | 78 | 98 (at 20°C avg) |
| IEC 60076-2 (Thermally Upgraded) | Mineral Oil | 60 | 65 | 78 | 110 |
| IEEE C57.12.00 (55°C Rise Paper) | Mineral Oil | 55 | 55 | 65 | 95 |
| IEEE C57.12.00 (65°C Rise Upgraded) | Mineral Oil | 65 | 65 | 80 | 110 |
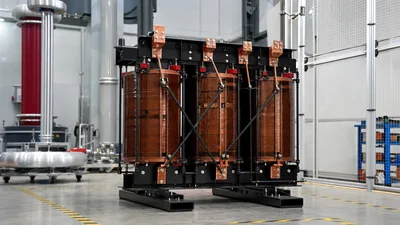
| IEC 60076-11 (Class F) | Dry-Type Cast Resin | N/A | 100 | 125 | 155 |
| IEC 60076-11 (Class H) | Dry-Type Cast Resin | N/A | 125 | 150 | 180 |
When reviewing factory design sheets, engineers must check whether values are expressed as absolute temperature in degrees Celsius (°C) or as thermal rise above ambient in Kelvin (K). Confusing these values during design review leads to incorrect winding conductor sizing and undersized cooling radiators.
How Transformer Winding Temperature Is Measured and Calculated
A standard winding temperature indicator does not physically touch the high-voltage winding; it reconstructs the temperature profile using a thermal replica method.
Because windings operate at potentials ranging from 11 kV to 500 kV and beyond, installing metallic wires directly into the coil assembly presents severe dielectric flashover risks. As a result, standard liquid-immersed transformers utilise an indirect measurement system. The primary monitoring technologies include:
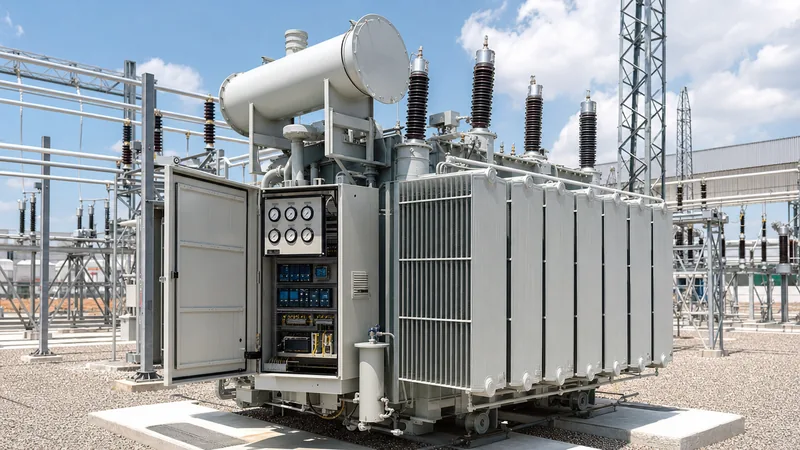
- Thermal Replica Indicators (Bourdon Tube WTI): A temperature-sensing bulb sits in a pocket (thermowell) in the top tank oil, picking up top oil temperature. This bulb connects via a capillary tube to a Bourdon gauge mechanism in the control cabinet. Inside the gauge, an auxiliary heating resistor coils around the thermal bellows. This heater receives secondary current proportional to load current from a current transformer (CT) located on the transformer bushing. The heater adds a temperature increment ($\Delta\theta_{w}$) to the top oil reading, causing the dial to display simulated transformer winding temperature.
- Fibre-Optic Direct Probes (FOT): Thin, dielectric gallium-arsenide (GaAs) or Fibre Bragg Grating (FBG) sensors are embedded directly between conductor turns and pressboard spacers during factory winding assembly. These immune-to-EMI glass sensors exit the tank through hermetic pass-through plates, providing instantaneous, real-time measurements of the actual winding hot-spot without thermal lag.
- PT100 Resistance Temperature Detectors (RTD): Common in dry type transformers, platinum RTDs are placed directly into the low-voltage windings where current density is highest, feeding signals into automated temperature monitoring controllers.
- Algorithmic Digital Twins: Integrated within modern substation transformer monitoring systems, computational software executes thermal models based on IEC 60076-7 or IEEE C57.91, taking ambient temperature, oil temperature, and load profiles to project real-time hot-spot conditions.
Conventional replica WTIs feature an inherent time lag of 15 to 45 minutes due to the thermal inertia of the pocket and oil. This lag makes them unsuitable for detecting sudden load surges on solar or wind farms, reinforcing the adoption of direct fibre optics on high-criticality assets.
Worked Calculation: Determining Hot-Spot Winding Temperature Under Overload
The winding hot-spot temperature ($T_{hs}$) is calculated using the standard thermal differential formula defined in IEC 60076-7 Clause 7.
Under steady-state conditions, the hot-spot temperature equals the sum of external ambient temperature, top oil temperature rise above ambient, and the winding hot-spot-to-top-oil thermal gradient:
$T_{hs} = T_a + \Delta\theta_{to} + \Delta\theta_{hs}$
Where:
- $T_a$ = Ambient air temperature (°C)
- $\Delta\theta_{to}$ = Top oil temperature rise above ambient (K)
- $\Delta\theta_{hs}$ = Hot-spot temperature rise above top oil temperature (K)
Consider a 25 MVA, 110/33 kV liquid-filled transformer operating under forced-air cooling (ONAF cooling regime). The factory heat-run test sheet confirms the following baseline parameters at rated load (1.0 p.u.):
- Rated Top Oil Rise ($\Delta\theta_{to,rated}$): 45 K
- Rated Hot-Spot Rise over Top Oil ($\Delta\theta_{hs,rated}$): 23 K
- Ratio of load losses to no-load losses ($R$): 6.0
- Oil thermal exponent ($x$): 0.8
- Winding thermal exponent ($y$): 1.6
Now, evaluate a summer overload scenario where the transformer carries 120% load ($K = 1.2$) at an external ambient temperature ($T_a$) of 35°C. The revised top oil rise is calculated using IEC 60076-7:
$\Delta\theta_{to} = \Delta\theta_{to,rated} \times \left( \frac{1 + R \times K^2}{1 + R} \right)^x$
$\Delta\theta_{to} = 45 \times \left( \frac{1 + 6.0 \times (1.2)^2}{1 + 6.0} \right)^{0.8} = 45 \times \left( \frac{1 + 8.64}{7.0} \right)^{0.8} = 45 \times (1.377)^{0.8} = 45 \times 1.291 = 58.1\text{ K}$
Next, determine the winding hot-spot-to-oil gradient under this 120% load:
$\Delta\theta_{hs} = \Delta\theta_{hs,rated} \times K^y = 23 \times (1.2)^{1.6} = 23 \times 1.339 = 30.8\text{ K}$
Sum the individual values to find the absolute hot-spot winding temperature:
$T_{hs} = 35°C + 58.1\text{ K} + 30.8\text{ K} = 123.9°C$
The calculated hot-spot of 123.9°C surpasses the standard 110°C continuous limit for thermally upgraded paper. Operating at this level subjects the asset to accelerated insulation ageing, demanding that substation operators either shed load or verify that the overload duration stays well within the permissible short-time thermal limits of IEC 60076-7 Table 4.
Impact of Excessive Transformer Temperature on Asset Life
Insulation ageing follows the classical Arrhenius chemical reaction rate, in which prolonged thermal excursion accelerates paper embrittlement and mechanical failure.
Solid cellulose insulation consists of long-chain glucose molecules. The mechanical strength of this paper is quantified by its Degree of Polymerisation (DP). Unprocessed, fresh kraft paper exhibits a DP value between 1,000 and 1,200. Throughout the normal operating life of a transformer, thermal stress, oxygen, and residual moisture break these polymer chains down. Once the DP drops to roughly 200 to 250, the mechanical tensile strength of the paper falls to below 20% of its original rating. At this point, known as the end-of-life criteria, normal electromechanical vibrations and short-circuit through-fault magnetic forces cause the paper to shatter, creating direct turn-to-turn dielectric breakdown.
The Montsinger Rule and IEEE C57.91 provide a quantitative rule of thumb: for every 6°C to 7°C increase in continuous operating hot-spot transformer temperature above design limits (e.g., above 110°C for thermally upgraded systems), the rate of insulation thermal ageing doubles, cutting expected service life by 50%.
Excessive thermal accumulation generates measurable chemical by-products that enter the insulating oil:
- Furanic Compounds: 2-Furfuraldehyde (2-FAL) forms almost exclusively from cellulose breakdown. Furan analysis via high-performance liquid chromatography (HPLC) gives engineers a direct chemical assessment of winding paper degradation without detanking the unit.
- Thermal Dissolved Gases: Dissolved Gas Analysis (DGA) per IEC 60599 reveals distinct gas profiles under thermal stress. Methane ($CH_4$) and ethane ($C_2H_6$) denote low-to-medium thermal faults ($<300°C$), while ethylene ($C_2H_4$) emerges as the dominant hydrocarbon gas when hot-spot temperatures push between 300°C and 700°C. High ratios of carbon monoxide ($CO$) and carbon dioxide ($CO_2$) confirm direct degradation of the solid paper insulation.
Protecting the winding from sustained thermal overshoots is the single most effective way to extend power transformer life past 30 to 40 operational years.
Thermal Management and Cooling Control Strategies
Cooling control systems manage thermal accumulation by switching cooling stages on and off in response to real-time top oil and winding temperature indicators.
Large distribution and power transformers use multi-stage cooling to adapt to shifting loads and changing ambient seasons. A standard multi-stage cooling unit relies on natural convection during low-load intervals, energising cooling fans and pumps as the winding thermals elevate. For an in-depth review of specific cooling stage switching circuits, refer to our detailed ONAF transformer cooling guide.
Automated thermal control relies on multi-contact auxiliary switches mounted within the mechanical WTI or programmed inside an electronic substation protection relay. Standard operational setpoints follow this sequence:
- Stage 1 Cooling (Fans Start): WTI reaches 65°C to 75°C. Cooling fan banks switch on to lower external radiator thermal resistance.
- Stage 2 Cooling (Pumps/Second Fan Bank Start): WTI reaches 75°C to 85°C. Forced-oil circulation pumps or secondary fan groups activate.
- Thermal Alarm: WTI reaches 105°C to 110°C. A supervisory warning transmits via SCADA to the central control room, signalling that the transformer is operating near its thermal limit.
- Thermal Trip: WTI reaches 120°C to 130°C. The trip contact triggers the master trip lockout relay (ANSI 86), commanding the high-voltage and low-voltage breakers to clear the transformer from the grid.
Integrating these thermal switches into complete substation trip matrices is outlined in our comprehensive transformer protection engineering guide. Modern installations also incorporate predictive cooling logic: rather than waiting for slow oil expansion to move a WTI dial, the digital controller samples breaker load current and activates fan banks proactively before winding temperatures rise.
Factory Acceptance Testing: Heat Run and Temperature Rise Verification
Manufacturers verify compliance with thermal performance guarantees through a factory heat-run test performed in accordance with IEC 60076-2 Clause 7 or IEEE C57.12.90 Clause 11.
The test uses the short-circuit method. The manufacturer shorts one winding set (usually the low-voltage side) while applying reduced voltage to the other side to circulate test currents. The test runs in two successive operational phases:
- Total Loss Injection: The test bay applies a combined test current representing total losses (no-load core losses plus rated load ohmic losses). This elevated input runs continuously until the top oil temperature rise stabilises at a rate of change under 1 K per hour over a consecutive three-hour period.
- Rated Current Injection: Once top oil rise is verified, the input power drops down to rated current ($1.0\text{ p.u.}$) for exactly one hour. This stabilises the true temperature gradient between the winding conductors and surrounding bulk oil.
- Shutdown and Resistance Extrapolation: Power is immediately cut, and test engineers rapidly connect Kelvin digital micro-ohmmeters to the winding terminals. Direct-current resistance measurements are recorded every 15 to 30 seconds for 10 to 15 minutes as the metal cools.
Because resistance cannot be safely measured while AC test power is connected, the cold-to-hot resistance change must be captured after shutdown. Since the winding begins cooling the moment power disconnects, engineers plot the cooling curve and extrapolate the resistance line back to the exact millisecond of shutdown ($t=0$) using mathematical regression per IEC 60076-2 Annex E.
The extrapolated resistance ($R_{hot}$) determines the average winding temperature ($\theta_w$) using the copper thermal coefficient equation:
$\theta_w = \frac{R_{hot}}{R_{cold}} \times (234.5 + \theta_{cold}) - 234.5$
For aluminium conductors, the constant 234.5 is replaced by 225.0. If the calculated winding temperature rise exceeds the client's guaranteed contract value by even 1 K, the manufacturer faces commercial penalties or redesign obligations.
Engineering Checklist for RFQs and Factory Specifications
A precise thermal engineering specification prevents common project delivery delays, miscalculated radiator sizing, and warranty disputes.
Project engineers, EPC contractors, and procurement teams should integrate the following technical requirements into their Request for Quotation (RFQ) packages when sourcing oil-immersed transformers or custom substations:
| Engineering Parameter | Specification Recommendation | Impact on Performance |
|---|---|---|
| Site Ambient Conditions | Specify maximum, monthly average, and annual mean ambient; state altitude if >1,000 m. | Prevents thermal de-rating; altitudes above 1,000 m reduce air density and cooling efficiency (IEC 60076-2 Clause 4.3). |
| Temperature Rise Limits | Mandate 55 K or 60 K winding rise instead of maximum allowed 65 K. | Lowering temperature rise limits provides built-in thermal reserve, allowing future overloads without degrading insulation. |
| Direct Fibre Optics (FOT) | Specify minimum 8 to 16 optical probes installed across all three phases on both HV and LV windings. | Removes WTI thermal lag; captures real-time hot spot for high-cycling renewable and data centre profiles. |
| WTI CT Matching | Require factory calibration sheet matching the heating element, CT ratio, and thermal gradient. | Prevents field errors where Bourdon WTI reads artificially high or low due to mismatched heater coils. |
| Radiator Corrosion Class | Specify ISO 12944 C4 or marine-grade paint coatings or hot-dip galvanised radiators. | Corroded cooling fins reduce heat dissipation and cause oil leaks, driving up internal winding temperatures. |
| Cooling Redundancy | Mandate $N-1$ fan redundancy on forced cooling stages. | Transformer retains 100% full rating even if one cooling fan or motor breaker fails in service. |
Next steps: specifying and sourcing
Procuring reliable power equipment requires aligning core-and-coil thermal design with site-specific duty cycles and environmental conditions. When preparing design briefs or tender packages, compile your project single-line diagrams, expected harmonic loading profiles, site ambient extremes, and cooling requirements. Our factory engineering team designs and manufactures utility-grade oil-immersed transformers, high-efficiency power transformers up to 110 kV, and specialised dry-type distribution equipment engineered to international standards. For technical support, custom thermal calculation models, or commercial project pricing, visit our contact page or submit your tender schedule directly via our request a quote portal.
Frequently asked questions
What is the normal winding temperature for a transformer?
Normal winding temperature for a standard mineral-oil transformer under full rated load operates between 85°C and 95°C at typical ambients. Continuous operation should remain below the design hot-spot limit of 98°C for standard paper, or 110°C for thermally upgraded cellulose insulation.
What is the difference between oil temperature and winding temperature?
Oil temperature measures the liquid dielectric gathered at the top of the tank, whereas winding temperature measures the actual copper or aluminium conductor inside the core assembly. Winding temperature is typically 15°C to 25°C hotter than top oil due to internal conductor losses.
Why does transformer winding temperature rise faster than oil temperature?
Windings have low thermal mass and generate heat directly from current flow, causing them to respond within minutes to sudden load increases. The large mass of insulating oil possesses high thermal inertia, taking several hours to heat up and reach equilibrium.
What causes high winding temperature in a transformer?
High winding temperature is caused by continuous overloads, severe harmonic distortion, elevated ambient air, blocked radiator cooling ducts, cooling fan failures, or sludge deposits restricting internal oil circulation. Internal turn-to-turn micro-faults also generate rapid, localised hot-spot spikes.
What is the trip limit for transformer winding temperature?
Standard trip limits for oil-immersed transformers are configured between 120°C and 130°C on the winding temperature indicator. Dry-type transformers with Class F insulation typically trip between 150°C and 155°C, while Class H dry-type units trip at 170°C to 180°C.
How does ambient temperature affect transformer temperature rise?
Ambient temperature acts as the thermal floor for heat dissipation. While the transformer temperature rise above ambient remains roughly constant for a fixed load, a higher ambient directly raises the absolute operational temperature, accelerating thermal paper degradation.
Tags: winding temperature transformer winding temperature transformer temperature rise transformer temp rise transformer cooling